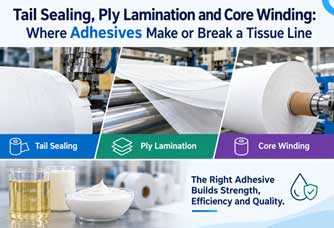
A tissue converting line can run at speed and still lose efficiency through poor bonding. Loose roll tails, weak ply adhesion and unstable cores can lead to product defects, rework and unnecessary downtime. For production managers and process engineers, understanding how adhesives behave at each stage is essential to maintaining consistent quality. Tail sealing, ply lamination and core winding each have different bonding requirements, and the right approach depends on the paper grade, machine conditions and demands placed on the finished roll.
Tail sealing: Securing the final sheet without damaging the roll
Tail sealing keeps the outermost sheet of a finished toilet tissue or paper towel roll in place. The bond must hold during handling, packaging and transport, while still allowing consumers to find and release the sheet without tearing away excessive paper.
Adhesive application is a balancing act. Too little adhesive, uneven coverage or poor contact between the tail and the underlying sheet can leave the roll loose. Excessive application, on the other hand, can create visible glue marks, stiff spots or a tail that is difficult to release. On automated lines, even small variations in application timing can affect several consecutive rolls before an operator notices the problem.
When tail seals fail, operators should check the complete application process rather than immediately increasing adhesive volume. Nozzle condition, adhesive temperature where applicable, application timing, tail position and the pressure applied during sealing can all affect the result. Paper dust and residue around the application point may also interfere with consistent delivery.
A useful troubleshooting method is to inspect defective rolls alongside acceptable ones. If the adhesive pattern differs, investigate the delivery system first. If the pattern looks consistent but the bond remains weak, check paper surface characteristics, contact conditions and whether the adhesive is suited to the application.
Ply lamination: Balancing bond strength with softness
Ply lamination joins two or more tissue layers to create a finished product with the desired thickness, appearance and handling characteristics. The adhesive must hold the plies together without making the paper feel stiff or compromising the embossing pattern.
The challenge is that tissue is lightweight and absorbent. An adhesive that performs well on a heavier paper grade may behave differently on a softer, more porous sheet. Application volume, viscosity, transfer method and the condition of the paper surface all influence how the adhesive spreads and forms a bond.
For production teams evaluating adhesives for tissue and towel converting, the key is to match the formulation and application method to the specific bonding task. A suitable adhesive must work with the line's operating conditions and the product's requirements, rather than being selected on bond strength alone.
Operators should pay attention to both bond consistency and finished-product feel. If the plies separate during rewinding or dispensing, check the adhesive transfer pattern and the alignment of the sheets. If the roll feels unusually stiff or develops visible marks, examine whether the adhesive is being applied too heavily or concentrated in the wrong areas.
Embossing can add another variable. The pressure and pattern used to join the plies affect the points of contact between sheets, so adhesive delivery must remain consistent with the converting process. Adjusting the adhesive without checking embossing pressure or alignment may address one symptom while leaving the underlying problem unresolved.
Core winding: Building a stable foundation for every roll
The core supports the finished tissue roll during winding, cutting, packaging and use. If the core is weak, poorly formed or dimensionally inconsistent, problems can appear downstream even when the tissue itself is converting correctly.
During core winding, adhesive bonds successive paper strips as they wrap around a mandrel. The bond must develop quickly enough to support continuous production while holding the layers together through winding and handling. The appropriate adhesive depends on factors such as paper characteristics, core construction, application equipment and line speed.
Adhesive distribution is particularly important. Uneven coverage can leave weak sections between layers, while excessive application may affect drying behaviour or create unwanted buildup on equipment. Operators should also monitor the condition of metering components and ensure that the adhesive supply remains consistent throughout a production run.
When cores split, deform or delaminate, the investigation should include more than adhesive selection. Check strip tension, winding pressure, paper alignment and the consistency of the incoming paper. Also inspect the core's dimensions and bonding pattern. A core that is not formed correctly may fail under load even if the adhesive itself is performing as intended.
Core winding also illustrates why adhesive performance cannot be assessed in isolation. The bond must suit the mechanical demands of the winding process and the requirements of the downstream rewinder. A core that appears sound immediately after production may still reveal weaknesses during subsequent handling.
Diagnosing adhesive problems across the converting line
Tail sealing, ply lamination and core winding are separate operations, but their problems can be difficult to distinguish when defects first appear. A loose finished roll, for example, could result from a failed tail seal, weak ply bonding or a core that cannot support the winding process.
A structured inspection helps narrow the cause. The TAPPI introduction to tissue converting treats core winding, ply bonding, rewinding and tail sealing as distinct parts of the converting process. This separation provides a practical starting point for troubleshooting each station against its own operating requirements.
Production teams can use a simple diagnostic sequence:
This approach is more reliable than making several adjustments simultaneously. Changing adhesive volume, temperature and machine pressure at once makes it difficult to identify which change resolved the problem.
Reliable bonding starts with process control
Adhesive performance on a tissue line depends on the relationship between formulation, application equipment, paper characteristics and machine settings. Tail sealing requires dependable closure, ply lamination needs consistent bonding without sacrificing product feel, and core winding must produce a stable structure that withstands downstream handling.
For manufacturers, the practical priority is to establish suitable operating conditions for each station and monitor them consistently. When defects occur, tracing the failure to its source helps reduce unnecessary adjustments, protect product quality and keep the converting line running reliably.

We use cookies to ensure you get the best experience on our website. Read more...