Infection control equipment has become an increasingly critical component of healthcare and pharmaceutical infrastructure, particularly as facilities face tighter expectations around contamination control, process consistency and workplace safety. Conventional fumigation and disinfection practices are steadily giving way to technologies that can deliver faster, more uniform and measurable outcomes across critical environments.
This shift has created demand for specialized infection control equipment manufacturers capable of combining engineering, microbiological efficacy and operational practicality. Radiant Innovations has built its business around this precise requirement.
Since its inception in 2003, the company has focused on bio-decontamination technologies for healthcare, pharmaceutical manufacturing and laboratory environments, developing equipment designed to address the limitations of conventional disinfection practices while improving process control and reproducibility.
Radiant Innovations began with an observation that continues to influence its product development approach: many existing disinfection methods were no longer aligned with the evolving requirements of critical environments. Traditional fumigation methods using formalin and potassium permanganate were time-consuming and carried limitations associated with their application. Similarly, equipment used for operation theatre disinfection and sterile-area treatment often left scope for improvement in terms of speed, safety, consistency and process control.
Rather than competing across the broader medical equipment landscape, Radiant Innovations chose to concentrate on the specialized field of airborne disinfection and bio-decontamination. This decision allowed the company to build deeper technical expertise around room-space treatment, surface coverage and microbial contamination control.
“Our early work involved developing alternative disinfection processes and subsequently designing and manufacturing specialized fogger systems using hydrogen peroxide-based disinfectants. Over time, this focused approach evolved into a wider portfolio of airborne disinfection systems, nebulized hydrogen peroxide dry-fog generators and pneumatic dry-fogging equipment. The company's contribution to the industry lies in this combination of specialization and indigenization.
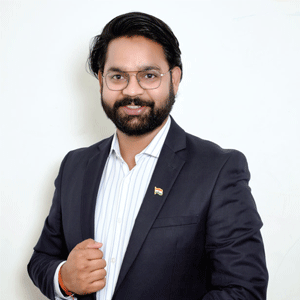
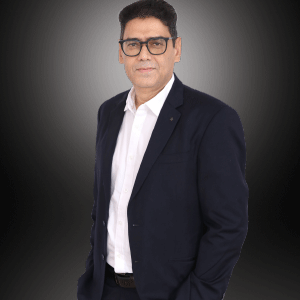
Its systems are developed for demanding environments where disinfection is not simply a routine cleaning activity but an integral part of contamination-control protocols. Hospitals, pharmaceutical manufacturing plants, microbiology laboratories, research facilities and sterile production areas therefore form an important part of its application landscape”, elaborates Parth Patel, Managing Partner.
From Disinfection Equipment to Complete Bio-Decontamination Solutions
Radiant Innovations' portfolio reflects its decision to remain focused on bio-decontamination rather than becoming a general-purpose equipment supplier. Its airborne disinfection systems include Aerojet Steriz, Yantra Automated and Rotofog, while the SATEJ range represents its work in nebulized hydrogen peroxide dry-fog technology.
Among these, the SATEJ 3Di has been developed for environments such as microbiology and tissue-culture laboratories, research institutes working in virology and immunology, pharmaceutical production areas, sterile facilities, injectable and vaccine manufacturing plants, and hospital operation theatres. Its 360-degree dry-fog distribution is designed to improve treatment of difficult-to-reach surfaces alongside more accessible areas, supporting a more uniform decontamination process.
The equipment also incorporates digital process control. The SATEJ 3Di uses a touchscreen HMI to facilitate controlled and reproducible treatment cycles, while process data can be retrieved for individual bio-decontamination treatments. Its design supports compliance requirements associated with 21 CFR Part 11, an important consideration for pharmaceutical and other regulated environments where electronic records and traceability matter.
The portfolio extends beyond automated systems. TRS 01, TRS 01 Flexible and TRS X are pneumatic-operated dry-fogging systems, while SATEJ SSD Ultra addresses small-space bio-decontamination. The SATEJ Handy Fog Disinfection Gun is designed for targeted surface treatment using nebulized fog, expanding the application of the technology to more localized requirements. Fogstar Pro, meanwhile, addresses indoor mosquito-control applications.
Across these products, the company places emphasis on robust construction and operational efficiency. Its equipment is manufactured using sanitary materials suitable for healthcare and pharmaceutical clean-room applications.
More importantly, Radiant Innovations positions its offerings as complete process solutions rather than simply machines. This distinction is central to its value proposition.
Making Bio-Decontamination More Controlled and Reproducible
For critical environments, the effectiveness of a disinfection system cannot depend solely on the equipment's ability to generate fog. The treatment cycle, dosage, distribution, contact conditions, validation and repeatability are equally important. Radiant Innovations has therefore built its product development around the need to make bio-decontamination more controlled and measurable.
The company's recipe-based systems are intended to simplify operation while supporting accurate and reproducible treatment cycles. Its SATEJ range takes this further through digitally controlled processes and retrievable treatment data. Such capabilities are particularly relevant to pharmaceutical and healthcare users, where demonstrating that a process has been performed consistently can be as important as the process itself.
Radiant Innovations also emphasizes microbiological validation of its disinfection processes. The objective is to move beyond equipment supply toward a more assured approach to room-space bio-decontamination, helping customers establish repeatable treatment protocols for their specific environments.
Quality considerations extend into manufacturing as well. The company's products and manufacturing facility are stated to have Quality Council of India approval, while its equipment carries CE certification for European customers. Its focus on sanitary-grade materials and clean-room-compatible design further reflects the expectations of the industries it serves.
Customer support forms another part of this model. Radiant Innovations focuses on installation quality, product and process-use training, after-sales assistance and timely availability of spares. For specialized contamination-control equipment, where incorrect installation or operation can undermine the intended outcome, this service orientation becomes a practical extension of the product itself.
Innovation Shaped by Customer Challenges
Radiant Innovations' approach to innovation is closely linked to the problems encountered by users in the field. Rather than treating product development as an isolated engineering exercise, the company continuously evaluates the strengths and limitations of its systems and uses customer requirements to identify areas for improvement.
This has helped it build a portfolio spanning automated airborne disinfection, dry-fog hydrogen peroxide systems, pneumatic equipment and targeted treatment devices. The company describes its team as solution-driven and customer-centric, with technical understanding of the environments in which its equipment operates.
That specialization is increasingly relevant as pharmaceutical and healthcare facilities seek greater control over contamination risks. The requirement is no longer simply to disinfect a room; users increasingly need processes that are consistent, documented, validated and suited to specific applications. Radiant Innovations' emphasis on reproducibility and process data positions its equipment accordingly.
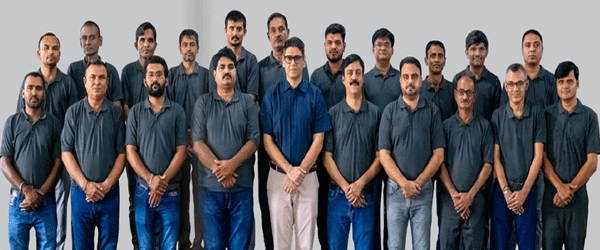
The company is also looking beyond its established applications. Its future development direction includes dry-vapour disinfection, smarter process controls and customized equipment designed around specific customer challenges. “An important objective is to achieve greater efficacy while reducing unnecessary chemical usage, creating systems that are safer and more environmentally conscious without compromising the effectiveness expected from professional bio-decontamination equipment”, adds Parth Patel.
Expanding the Contamination-Control Horizon
The next phase of Radiant Innovations' growth is centred on strengthening both its technology base and market reach. The company plans to improve the performance of its existing systems while developing new equipment capable of meeting stricter compliance and microbial-validation requirements for room-space bio-decontamination.
Small-space bio-decontamination is another area of focus, alongside specialized equipment for targeted treatment of objects and surfaces. These developments could broaden the applicability of bio-decontamination technologies beyond conventional large-room applications and address more specific contamination-control requirements. Radiant Innovations' portfolio reflects its decision to remain focused on bio-decontamination rather than becoming a general-purpose equipment supplier
“Market expansion will also remain important. Radiant Innovations intends to deepen its presence across Indian healthcare and pharmaceutical markets while increasing its reach in export markets. At the same time, the company is evaluating opportunities in food processing, dairy and hatchery applications, where large-space disinfection can play a significant role in maintaining hygienic production environments”, speaks Parth Patel.
Underpinning this roadmap is a commitment to strengthening its technical team and reinvesting in research and development. The company intends to continue refining existing systems, developing new solutions and using data-driven process validation to improve performance. Its longer-term ambition is to evolve from an equipment manufacturer into a comprehensive contamination-control partner capable of addressing different scales and applications of bio-decontamination.
The recognition amongst Emerging Player in Bio-decontamination Equipment Manufacturer therefore comes at a significant point in Radiant Innovations' journey. For a company that began by identifying shortcomings in conventional disinfection practices, its progress reflects the value of sustained specialization and application-led engineering.
As healthcare and pharmaceutical facilities place greater emphasis on controlled, validated and reproducible contamination-control processes, Radiant Innovations is positioning itself to participate in that transition - not merely by supplying equipment, but by developing technologies and processes designed around the realities of critical environments.


We use cookies to ensure you get the best experience on our website. Read more...